White paper
Sustainability benefits of Near-Infrared (NIR) integrated powder blending in pharmaceutical manufacturing.
-
Reading time 7 min
-
A study by
-
Exclusively for
COM.PACK
Introduction
In modern pharmaceutical manufacturing, particularly in the production of Oral Solid Dosage (OSD) forms, powder blending represents a critical unit operation. Blend homogeneity directly impacts critical quality attributes (CQAs) such as content uniformity, dose accuracy, and ultimately patient safety. At the same time, blending is traditionally associated with significant process time, repeated off-line quality control (QC) testing, and material consumption for sample withdrawal and destructive analysis.
These aspects translate into increased energy usage, material waste, and operational inefficiencies.
The integration of Near-Infrared (NIR) spectroscopy as an in-line Process Analytical Technology (PAT) within powder blending operations fundamentally changes this paradigm. By enabling real-time, non-destructive, and continuous monitoring of blend homogeneity, NIR-based systems support a scientific, data-rich approach to process understanding and control, aligned with Quality by Design (QbD) and regulatory expectations.
In particular, this approach is fully consistent with the principles outlined in ICH Q8 (Pharmaceutical Development), ICH Q9 (Quality Risk Management), and ICH Q10 (Pharmaceutical Quality System), as well as the FDA Guidance on PAT.
These frameworks explicitly encourage enhanced process understanding, real-time monitoring, and life-cycle process verification as mechanisms to ensure product quality while improving manufacturing efficiency.
Beyond quality and compliance, the adoption of NIR-based in-line monitoring delivers measurable sustainability benefits through reductions in processing time, energy consumption, downstream QC activities, solvent usage, and material waste. These benefits directly contribute to corporate Environmental, Social, and Governance (ESG) objectives by supporting energy efficiency, waste minimisation, and responsible resource utilization within GMP manufacturing environments.
IMA approach
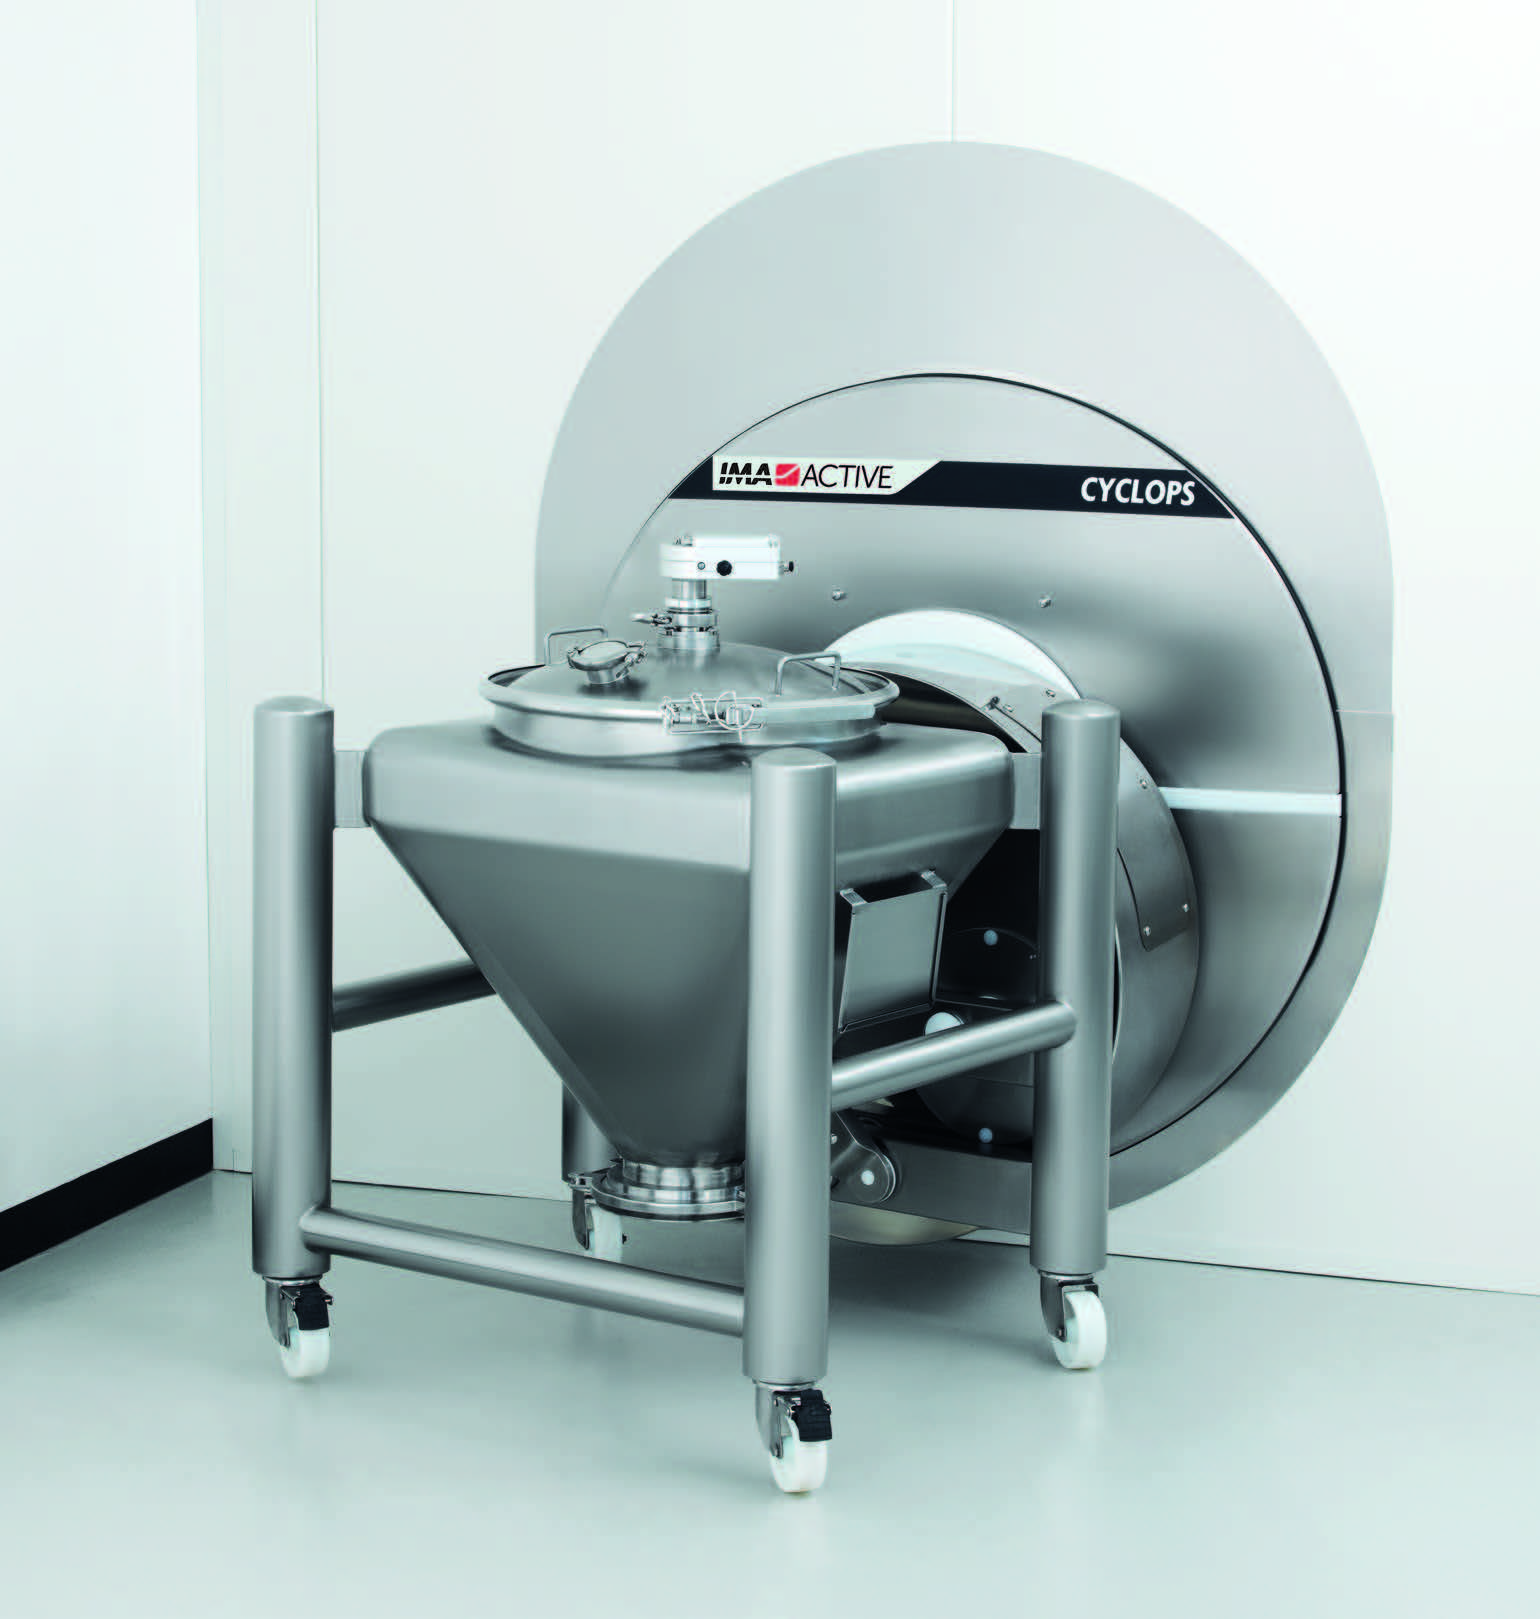
The use of an in-line MicroNIR spectrometer in IMA blenders demonstrates how the use of NIR spectroscopy in pharmaceutical powder blending enhances process sustainability through process time optimisation, energy efficiency, and reduction of analytical and material burdens.
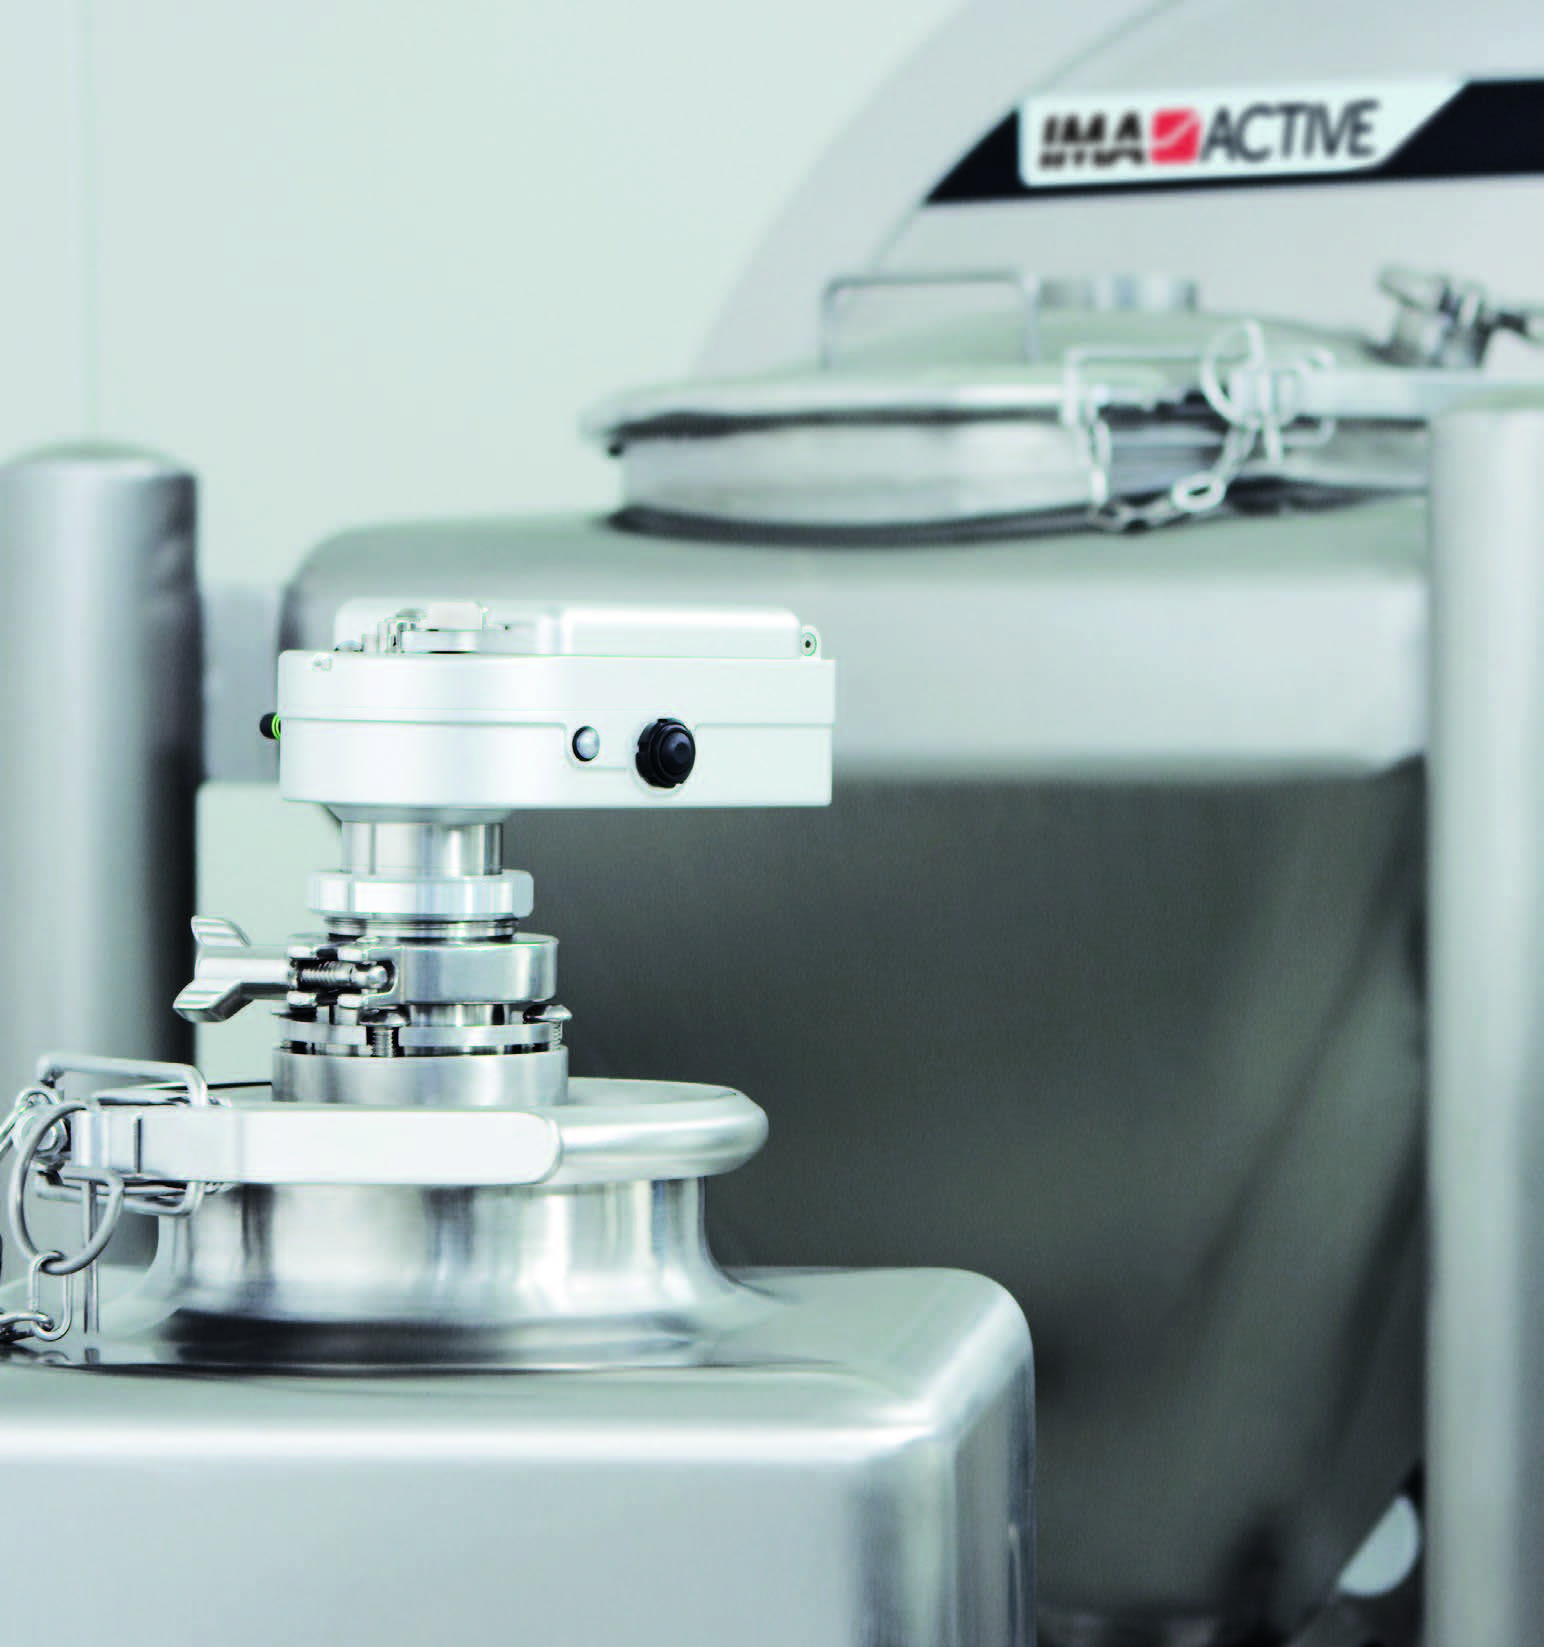
When implemented in-line on a tumble blender, such as the CYCLOPS LAB system, the MicroNIR sensor continuously acquires spectral data throughout the entire blending operation.
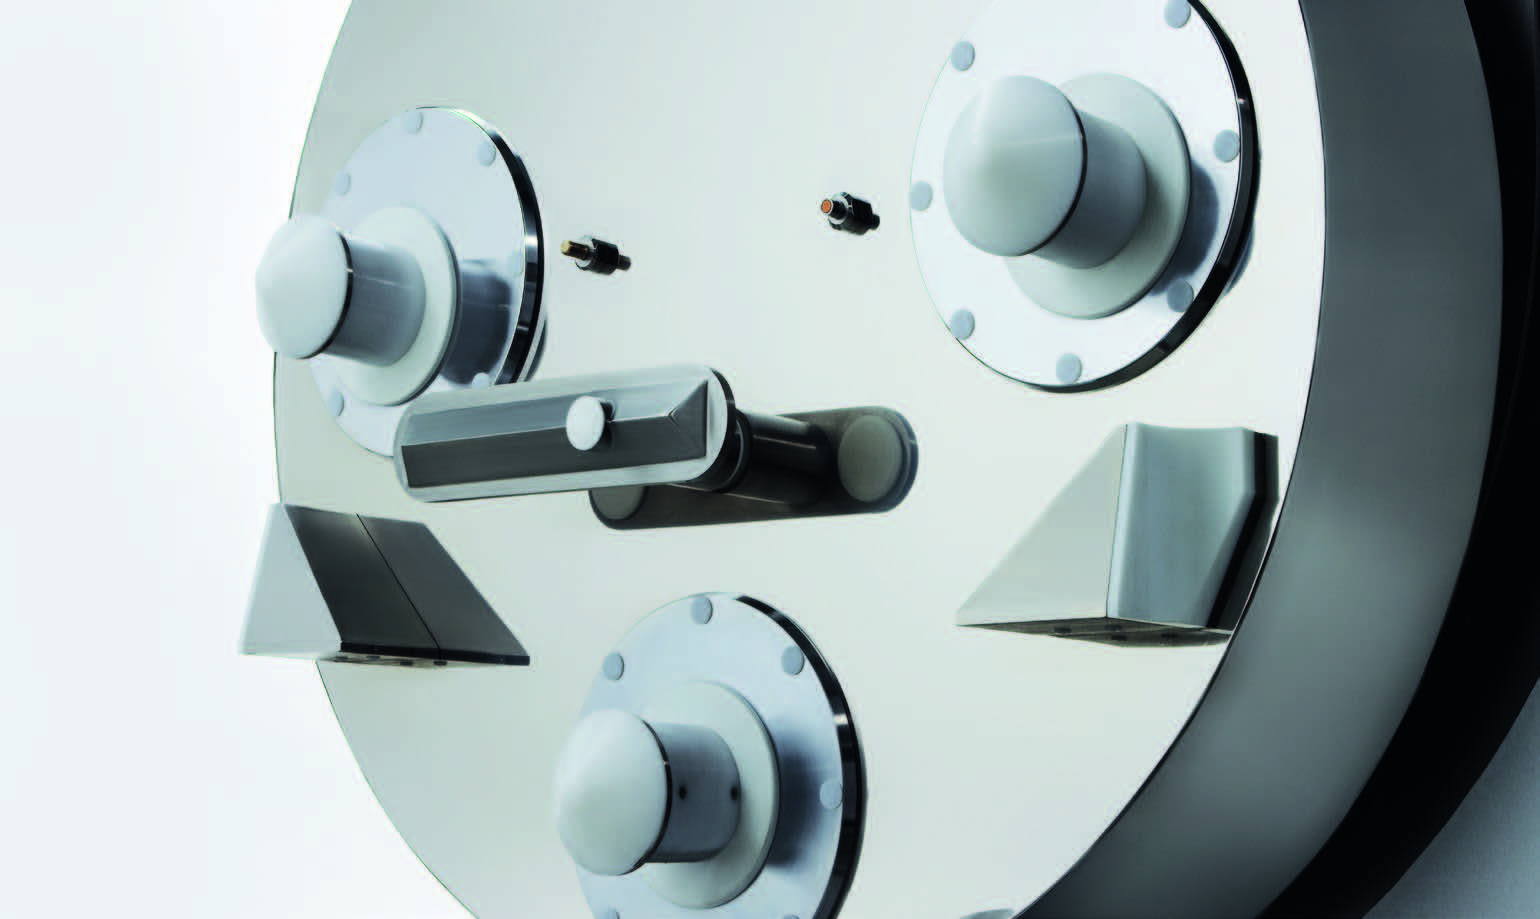
This small device is clamped on the bin lid through a tailored sight-glass flange, enabling uninterrupted acquisition under real operational conditions.
This configuration is inherently non-invasive and does not introduce any mechanical or thermal perturbation to the system.
A key mechanism by which in-line NIR monitoring enables tangible reduction of blending time is the application of chemometric analysis based on the Moving Block Standard Deviation (MBSD) of the acquired spectral data. Unlike conventional end-point determination methods, which rely on fixed processing times or off-line sampling, MBSD provides a statistically robust indicator of blend homogeneity derived directly from in-process spectral variability.
From a mathematical standpoint, MBSD quantifies the local standard deviation of NIR spectra with respect to blending time. During the early stages of blending, high MBSD values are typically observed due to heterogeneous distribution of formulation components and pronounced spectral variability. As mixing progresses, particle redistribution and improved component dispersion lead to a progressive reduction in spectral variability, which is reflected by a decreasing MBSD trend, as clearly visible in the experimental graphs reported below.
The critical advantage of MBSD analysis lies in its ability to identify, in real time, the transition from an active mixing regime to a steady-state homogeneous condition. When the MBSD profile reaches a stable minimum or plateau, further blending does not produce any statistically significant improvements in homogeneity. At this point, continued operation of the blender represents overprocessing, contributing only to additional energy consumption, mechanical stress, systematic overmixing and even potential demixing.
Moreover, through MBSD analysis, minor behavioral differences among similar formulations can be detected and the process can be optimised accordingly. Graph 1 shows the experimental data of blending processes obtained with two formulations differing only in the PSD of microcrystalline cellulose.
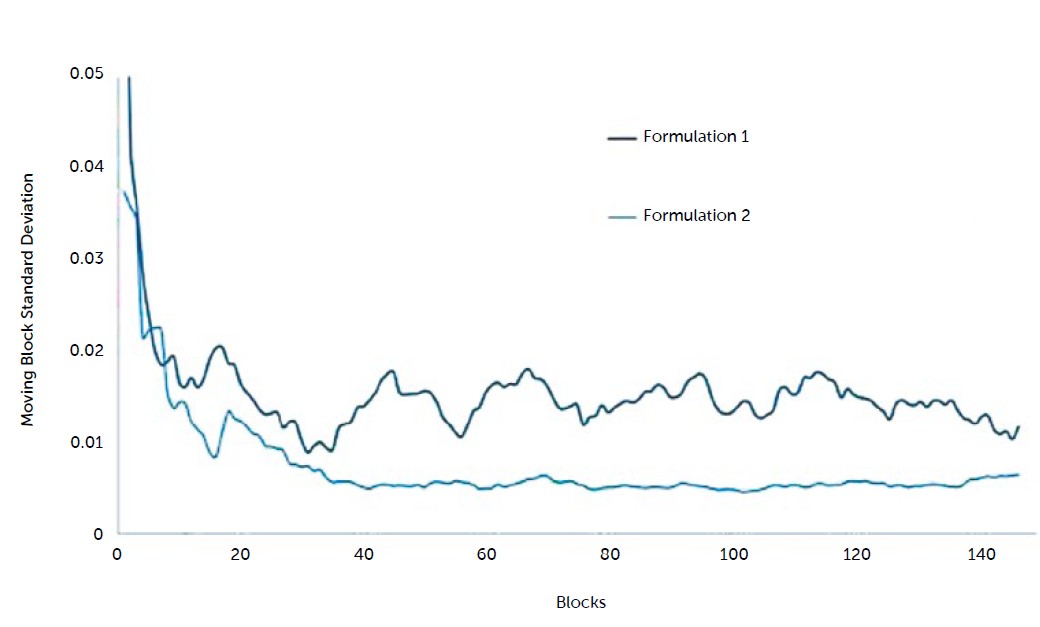
Graph 1: MBSD profiles obtained on CYCLOPS LAB under identical blending conditions: bin filling 75%. Formulation 1 and Formulation 2 are blends containing microcrystalline cellulose PH101 and PH102 respectively.
These similar blends exhibit distinct MBSD decay kinetics under identical process conditions demonstrating that a fixed blending time would inevitably overprocess at least one of the two formulations, whereas MBSD-based monitoring enables formulation-specific endpoint determination.
Similarly, Graph 2 highlights how MBSD-based monitoring allows the best equipment set-up for each formulation.
By enabling objective, data-driven identification of the MBSD plateau, chemometric analysis allows batch-specific and formulation-specific determination of the true blending endpoint. This approach replaces conservative, worst-case mixing times with scientifically justified, real-time decisions, fully aligned with PAT and Quality by Design principles.
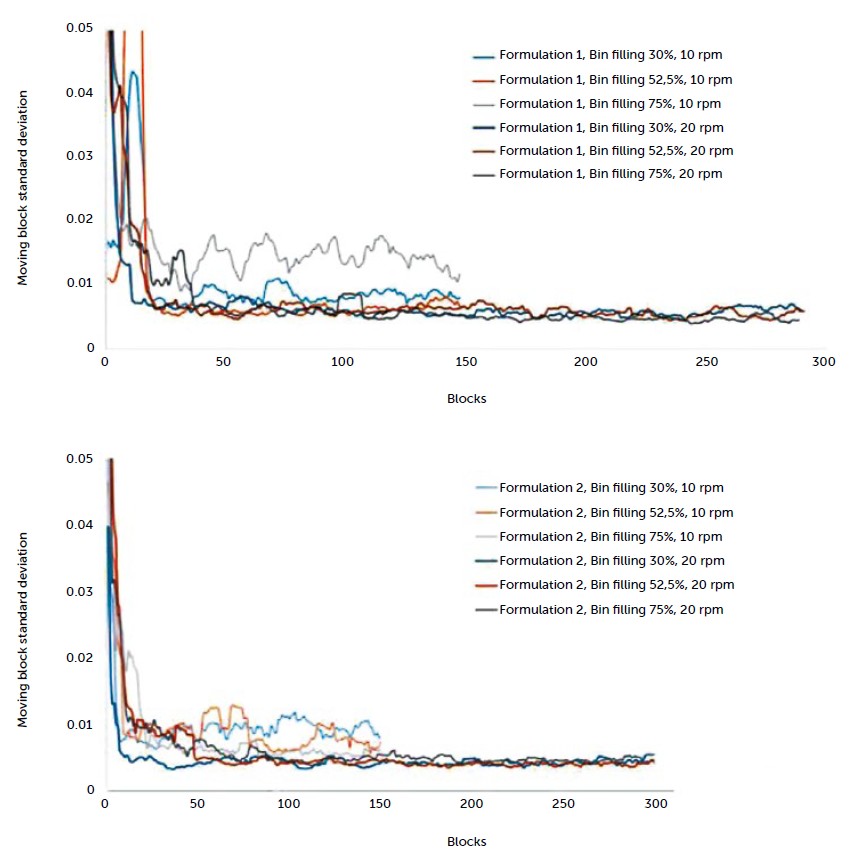
Graph 2: MBSD profiles obtained on CYCLOPS by varying the bin filling level and the rpm for both Formulation 1 and Formulation 2.
Sustainability pillars
Blending equipment energy consumption is directly proportional to operating time and mechanical load. By reducing blending time through real-time MBSD endpoint detection, NIR implementation leads to lower electrical energy demand per batch; reduced mechanical wear on motors, bearings, and drive systems; and decreased heat generation, with secondary benefits on HVAC requirements in GMP areas.
In high-frequency batch or Continuous Manufacturing environments, even single-digit percentage reductions in blending duration can lead to substantial annual energy savings and associated reductions in CO₂ emissions. These cumulative benefits significantly strengthen the justification for NIR-based PAT implementation from both an economic and environmental sustainability perspective. Moreover, conventional assessment of blend uniformity relies on off-line sampling followed by wet chemistry analysis, typically high-performance liquid chromatography (HPLC). This approach requires: physical sampling of the blend (often multiple locations); sample preparation using solvents and consumables; destructive analysis and waste disposal; significant analyst time and laboratory energy use.
In contrast, in-line NIR monitoring provides a continuous, batch-representative assessment of homogeneity without removing material from the process.
This contributes to sustainability through lower consumption of solvents and reagents used in wet chemistry; reduced use of vials, filters, columns, and disposable laboratory plastics; elimination of blend material wasted for analytical purposes. Furthermore, as NIR analysis is non-destructive, 100% of the batch remains available for downstream processing, improving overall material yield. From an operational perspective, reduced reliance on off-line QC shortens release times and minimises work-in-progress inventory. This has indirect sustainability benefits by: reducing storage requirements and associated energy use; improving manufacturing scheduling and equipment utilisation; lowering the probability of batch rework or rejection due to late detection of blend non-uniformity. Beyond direct time and energy savings, NIR-based blending control enhances overall process robustness. Continuous monitoring allows early detection of atypical blending behavior caused by raw material variability or equipment deviations. Corrective actions can be taken before non-conforming material proceeds further in the process chain. By preventing failures (out-of-specification product), NIR-supported blending aligns strongly with the principles of sustainable manufacturing.
Conclusions
The integration of NIR spectroscopy into pharmaceutical powder blending processes provides clear and scientifically substantiated sustainability benefits. Real-time, in-line monitoring enables accurate determination of blending endpoints, leading to reduced process time and lower energy consumption. Simultaneously, the shift from off-line to in-process quality assessment minimises the need for destructive testing, cutting down on analytical materials, solvents, and waste. The experimental evidence from the CYCLOPS blending case study demonstrates that NIR-based MBSD analysis reliably captures blending dynamics and correlates with traditional quality metrics. By embedding this capability into routine production, manufacturers can achieve a more efficient, robust, and environmentally responsible process without compromising product quality or regulatory compliance. In the context of increasing regulatory emphasis on PAT, QbD, and sustainable manufacturing, NIR-enabled blending represents a mature and high-impact technological solution that directly supports both operational excellence and long-term sustainability goals.
CYCLOPS

4 min
Brands: IMA North America Inc. – Thomas Division, IMA Active
White paper
Effervescent tablet processing and packaging: why integrated lines are shaping the future.
6 min
Brands: IMA S.p.A. – Active Division, IMA Active
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
ARCA: AI Root Cause Analysis.
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
AMIX Nutrition and IMA Active: technological evolution supporting next generation sports nutrition.
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
13 min
Brands: IMA S.p.A. – Active Division, IMA Active
5 min
Brands: IMA S.p.A. – Active Division, IMA Active
7 min
Brands: IMA S.p.A. – Active Division, IMA Active
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
6 min
Brands: IMA S.p.A. – Active Division, IMA Active
12 min
Brands: IMA S.p.A. – Active Division
11 min
Brands: IMA Active, IMA S.p.A. – Active Division
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
11 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Vitabalans Oy chooses PREXIMA.
4 min
Brands: IMA Active, IMA S.p.A. – Active Division
16 min
Brands: IMA S.p.A. – Active Division, IMA Active
12 min
Brands: IMA S.p.A. – Active Division, IMA Active
9 min
Brands: IMA S.p.A. – Active Division, IMA Active
25 min
Brands: IMA S.p.A. – Active Division, IMA Active
20 min
Brands: IMA S.p.A. – Active Division, IMA Active
20 min
Brands: IMA S.p.A. – Active Division, IMA Active
White paper
The Energy Diary: powering sustainability.
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
10 min
Brands: IMA Active, IMA S.p.A. – Active Division
4 min
Brands: IMA Active, IMA North America Inc. – Thomas Division, IMA S.p.A. – Active Division
12 min
Brands: IMA Active, IMA S.p.A. – Active Division
8 min
Brands: IMA S.p.A. – Active Division, IMA Active
10 min
Brands: IMA S.p.A. – Active Division, IMA Active
10 min
Brands: IMA Active, IMA S.p.A. – Active Division
14 min
Brands: IMA Active, IMA S.p.A. – Active Division
6 min
Brands: IMA S.p.A. – Active Division, IMA Active
11 min
Brands: IMA S.p.A. – Active Division, IMA Active
6 min
Brands: IMA S.p.A. – Active Division, IMA Active
14 min
Brands: IMA S.p.A. – Active Division, IMA Active
15 min
Brands: IMA S.p.A. – Active Division, IMA Active
10 min
Brands: IMA S.p.A. – Active Division, IMA Active
17 min
Brands: IMA S.p.A. – Active Division, IMA Active
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
12 min
Brands: IMA S.p.A. – Active Division, IMA Active
13 min
Brands: IMA Active, IMA S.p.A. – Active Division
11 min
Brands: IMA Active, IMA S.p.A. – Active Division
11 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
Influence of material and capsule filling process with Minima on aerosolization performances by DPIs.
12 min
Brands: IMA Active, IMA S.p.A. – Active Division
10 min
Brands: IMA Active, IMA S.p.A. – Active Division
6 min
Brands: IMA S.p.A. – Active Division, IMA Active
Case study
Algorithm: «Why we choose IMA».
3 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Tablets: the importance of uniform coating.
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
IMA Active drives forward the successful uptake of Continuous Manufacturing in the pharmaceutical industry.
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
18 min
Brands: IMA S.p.A. – Active Division, IMA Active
18 min
Brands: IMA Active, IMA S.p.A. – Active Division
30 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA S.p.A. – Active Division, IMA Active
4 min
Brands: IMA S.p.A. – Active Division, IMA Active
Case study
Mastering tablet manufacturing: how segment tools improve productivity, efficiency and consistency.
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
34 min
Brands: IMA Active, IMA S.p.A. – Active Division
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
2 min
Brands: IMA Active, IMA S.p.A. – Active Division
11 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
Comparison of minitablets and pellets as multiparticulate drug delivery systems for controlled drug release.
24 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Lubricant sensitivity of direct compression grades of lactose in continuous batch tableting process.
33 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
9 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
Component washing: better with less.
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
New solutions for nutraceuticals.
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
17 min
Brands: IMA Active, IMA S.p.A. – Active Division
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
14 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Food supplement revolution.
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
CROMA continuous coater: saving energy and process time by using high solids coating material.
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Application of acrylic enteric coating directly on soft gelatine capsules using a GS coating pan.
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
8 min
Brands: IMA S.p.A. – Active Division, IMA Active
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
11 min
Brands: IMA Active, IMA S.p.A. – Active Division
12 min
Brands: IMA Active, IMA S.p.A. – Active Division
9 min
Brands: IMA Active, IMA S.p.A. – Active Division
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
Formulating tablets layer by layer.
10 min
Brands: IMA Active, IMA S.p.A. – Active Division
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Formulation development of Vitamin C based effervescent blend suitable for direct compression.
9 min
Brands: IMA Active, IMA S.p.A. – Active Division
9 min
Brands: IMA Active, IMA S.p.A. – Active Division
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Extrusion-Molding-Coating process advantages for Continuous Manufacturing of oral solid dosage forms
12 min
Brands: IMA Active, IMA S.p.A. – Active Division
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
13 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
Autoregulation function on DOMINA tablet press.
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
The potential of CROMA continuous coater.
9 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
IMA Coffee partners with Smile Beverage Werks to produce new, sustainable single-serve capsules
7 min
Brands: IMA S.p.A. – Coffee Division, IMA Active, IMA S.p.A. – Active Division
White paper
Perfima Extra: your way to boost productivity keeping process quality at the highest standard.
4 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
IMA and OSIsoft: setting the standard in table process data to accelerate production setup.
5 min
Brands: IMA S.p.A. – Active Division, IMA Active
9 min
Brands: IMA S.p.A. – Active Division, IMA Active
10 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
10 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Power to the essential.
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Much more than nutraceuticals.
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
Preliminary results of predictive maintenance algorithms on a tablet press production machine.
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
The Prexima challenge. Comparison of rotary tablet presses seminar in Leverkusen (Germany).
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Directly compressed minitablets coated in a solid wall pan for the sustained release of drugs.
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
ARIA fluid bed granulator and MicroNIR
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
CYCLOPS. Blending made by IMA.
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
The IMA Group integrates OMAC PackML and invests in the future of machine connection and control.
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
How to perform a good scale-up.
6 min
Brands: IMA S.p.A. – Active Division, IMA Active
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
29 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Drug layering: the impact of up-scaling.
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
10 min
Brands: IMA Active, IMA S.p.A. – Active Division
15 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Scaling up a film coating process.
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
Manufacturing DPIs: an engineering perspective
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
Salty compression.
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
4 min
Brands: IMA Active, IMA S.p.A. – Active Division
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
High Containment in OSD
7 min
Brands: IMA Active, IMA Safe, IMA S.p.A. – Safe Division, IMA S.p.A. – Active Division
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
9 min
Brands: IMA Active
Case study
Tableting at its best.
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
3 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
GlaxoSmithKline chooses PERFIMA.
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Design ad Hoc. Delpharm chose EFFECTA.
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Together again: Chinoin chooses IMA.
4 min
Brands: IMA Active, IMA S.p.A. – Active Division
4 min
Brands: IMA Active, IMA S.p.A. – Active Division
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
BMP: «PREXIMA fits all our needs».
4 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Fine Foods: «Why we choose IMA».
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Leading the way in micro-dosing DPIs.
6 min
Brands: IMA Active, IMA S.p.A. – Active Division