White paper
Effervescent tablet processing and packaging: why integrated lines are shaping the future.
-
Reading time 6 min
-
A study by
Introduction
Effervescent tablets continue to rise in popularity in the global pharmaceutical landscape. Demand is driven by several factors: patient preference for easy-to-take dosage forms, fast dissolution and absorption and the growing use of OTC products such as vitamins, electrolytes and cold-and-flu remedies. As consumption increases, manufacturers face rising pressure to achieve higher production speeds, undisputed quality and uncompromising moisture protection, all while maintaining cost-efficient operations.
This evolution has accelerated the need for fully integrated, high-performance processing and packaging lines specifically designed for effervescent applications.
In this scenario, equipment suppliers capable of providing seamless end-to-end solutions have become essential partners for leading pharmaceutical producers. IMA stands out as a single-source supplier offering a complete line for effervescent tablet processing and packaging. With technologies covering every phase, from powder compression to final packaging, IMA ensures reliability and production continuity while simplifying project execution.
A portfolio of technologies for every step
IMA’s integrated lines are powered by an extensive cross-divisional machine portfolio, enabling tailored configurations that match customer production targets, regulatory and operational needs.
Oral Solid Dose Processing – IMA Active
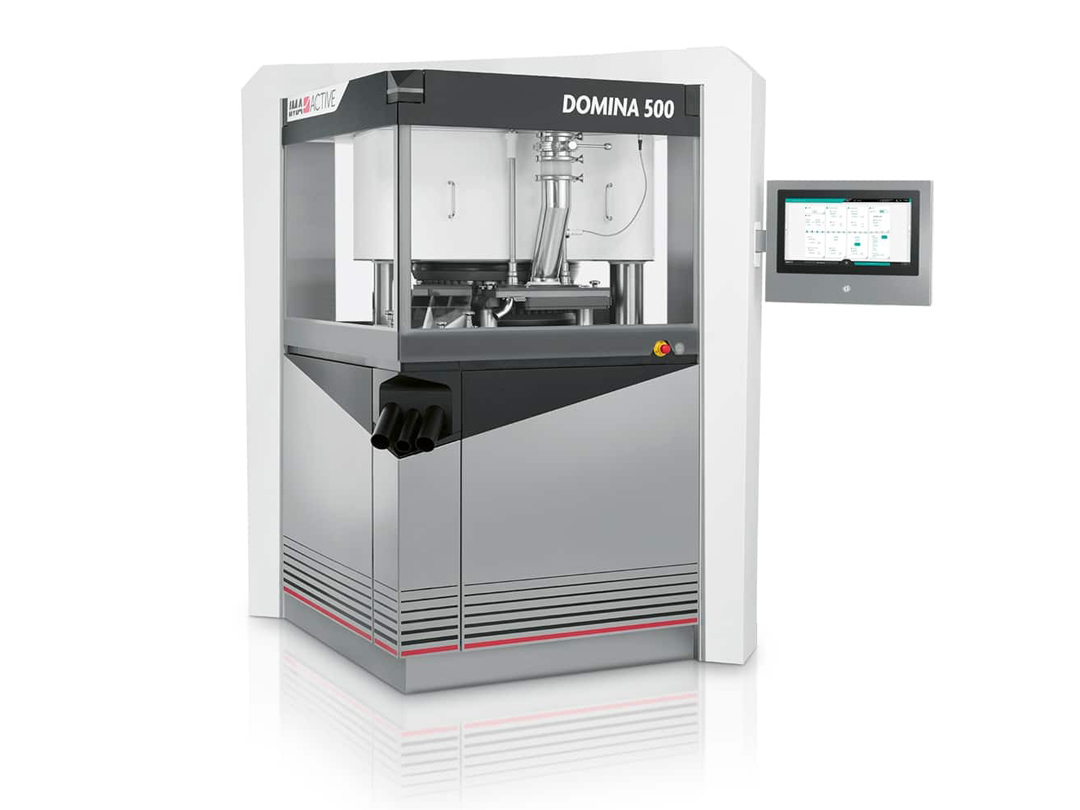
Effervescent tablets require exceptional mechanical stability, accurate weight control and tight moisture management. These constraints make the compression stage a critical step in the effervescent workflow. IMA Active meets these requirements with the entire tableting portfolio: PREXIMA, SOLIDA and DOMINA.
These tablet presses are engineered to ensure robust performance, reliability and consistent product quality even when processing highly sensitive formulations. DOMINA builds on IMA’s proven expertise in solid dose technologies and is part of a broader portfolio covering every step of the process, from powder handling to final compression.
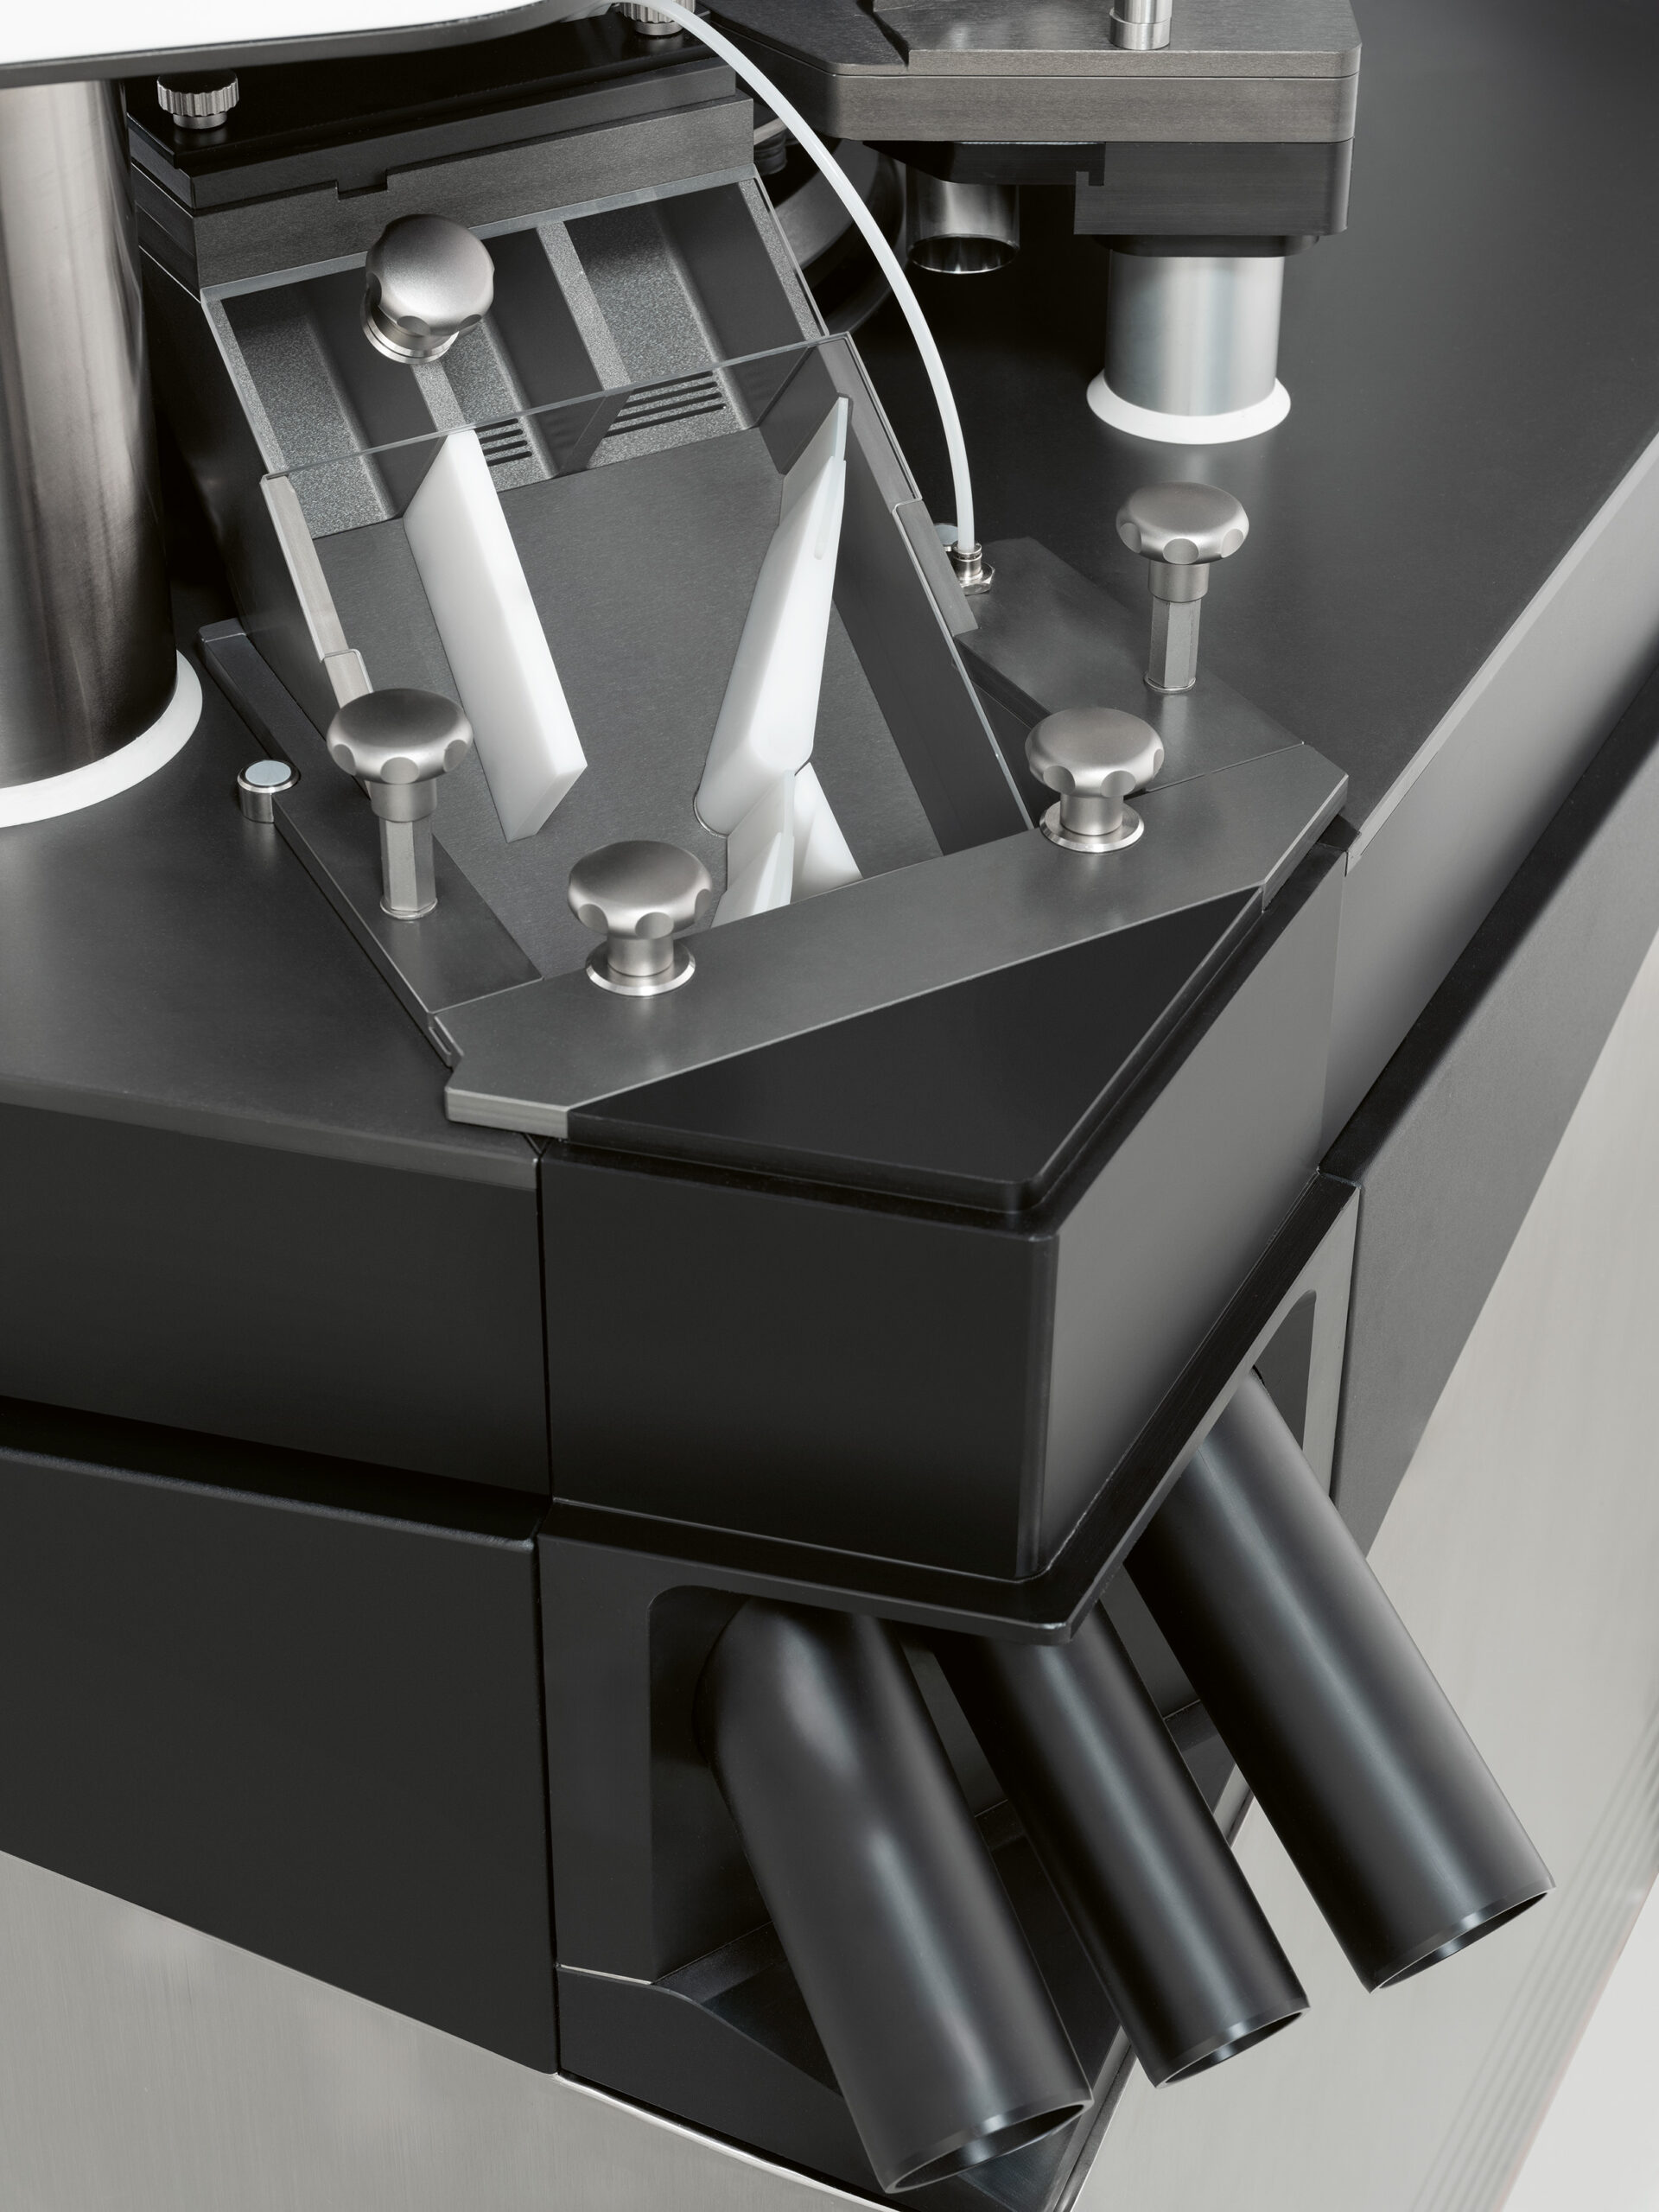
Thanks to its rigid structure, complete separation between mechanical and processing areas and advanced control systems, DOMINA ensures uniform compression, minimal weight variation and stable high-speed operation.
This makes it ideally suited to effervescent applications, where tablets must dissolve quickly while maintaining mechanical strength throughout downstream handling. DOMINA supports both single-layer and complex tablet configurations and delivers fast, intuitive changeover procedures to support high-throughput environments. Upstream of compression, effervescent manufacturing requires granulation processes capable of delivering powders with controlled moisture content, good-to-excellent flowability and high uniformity. Drawing on decades of experience, IMA Active supports this step with a dedicated set of granulation technologies, such as ROTO CUBE, that ensure stable and processable material for effervescent formulations.
These solutions enable the production of granulates with consistent particle size distribution, rapid solubility and the mechanical properties required for downstream tableting. By delivering reliable, stable powders, IMA Active strengthens the overall performance and continuity of effervescent production lines.

Secondary Packaging – IMA Safe
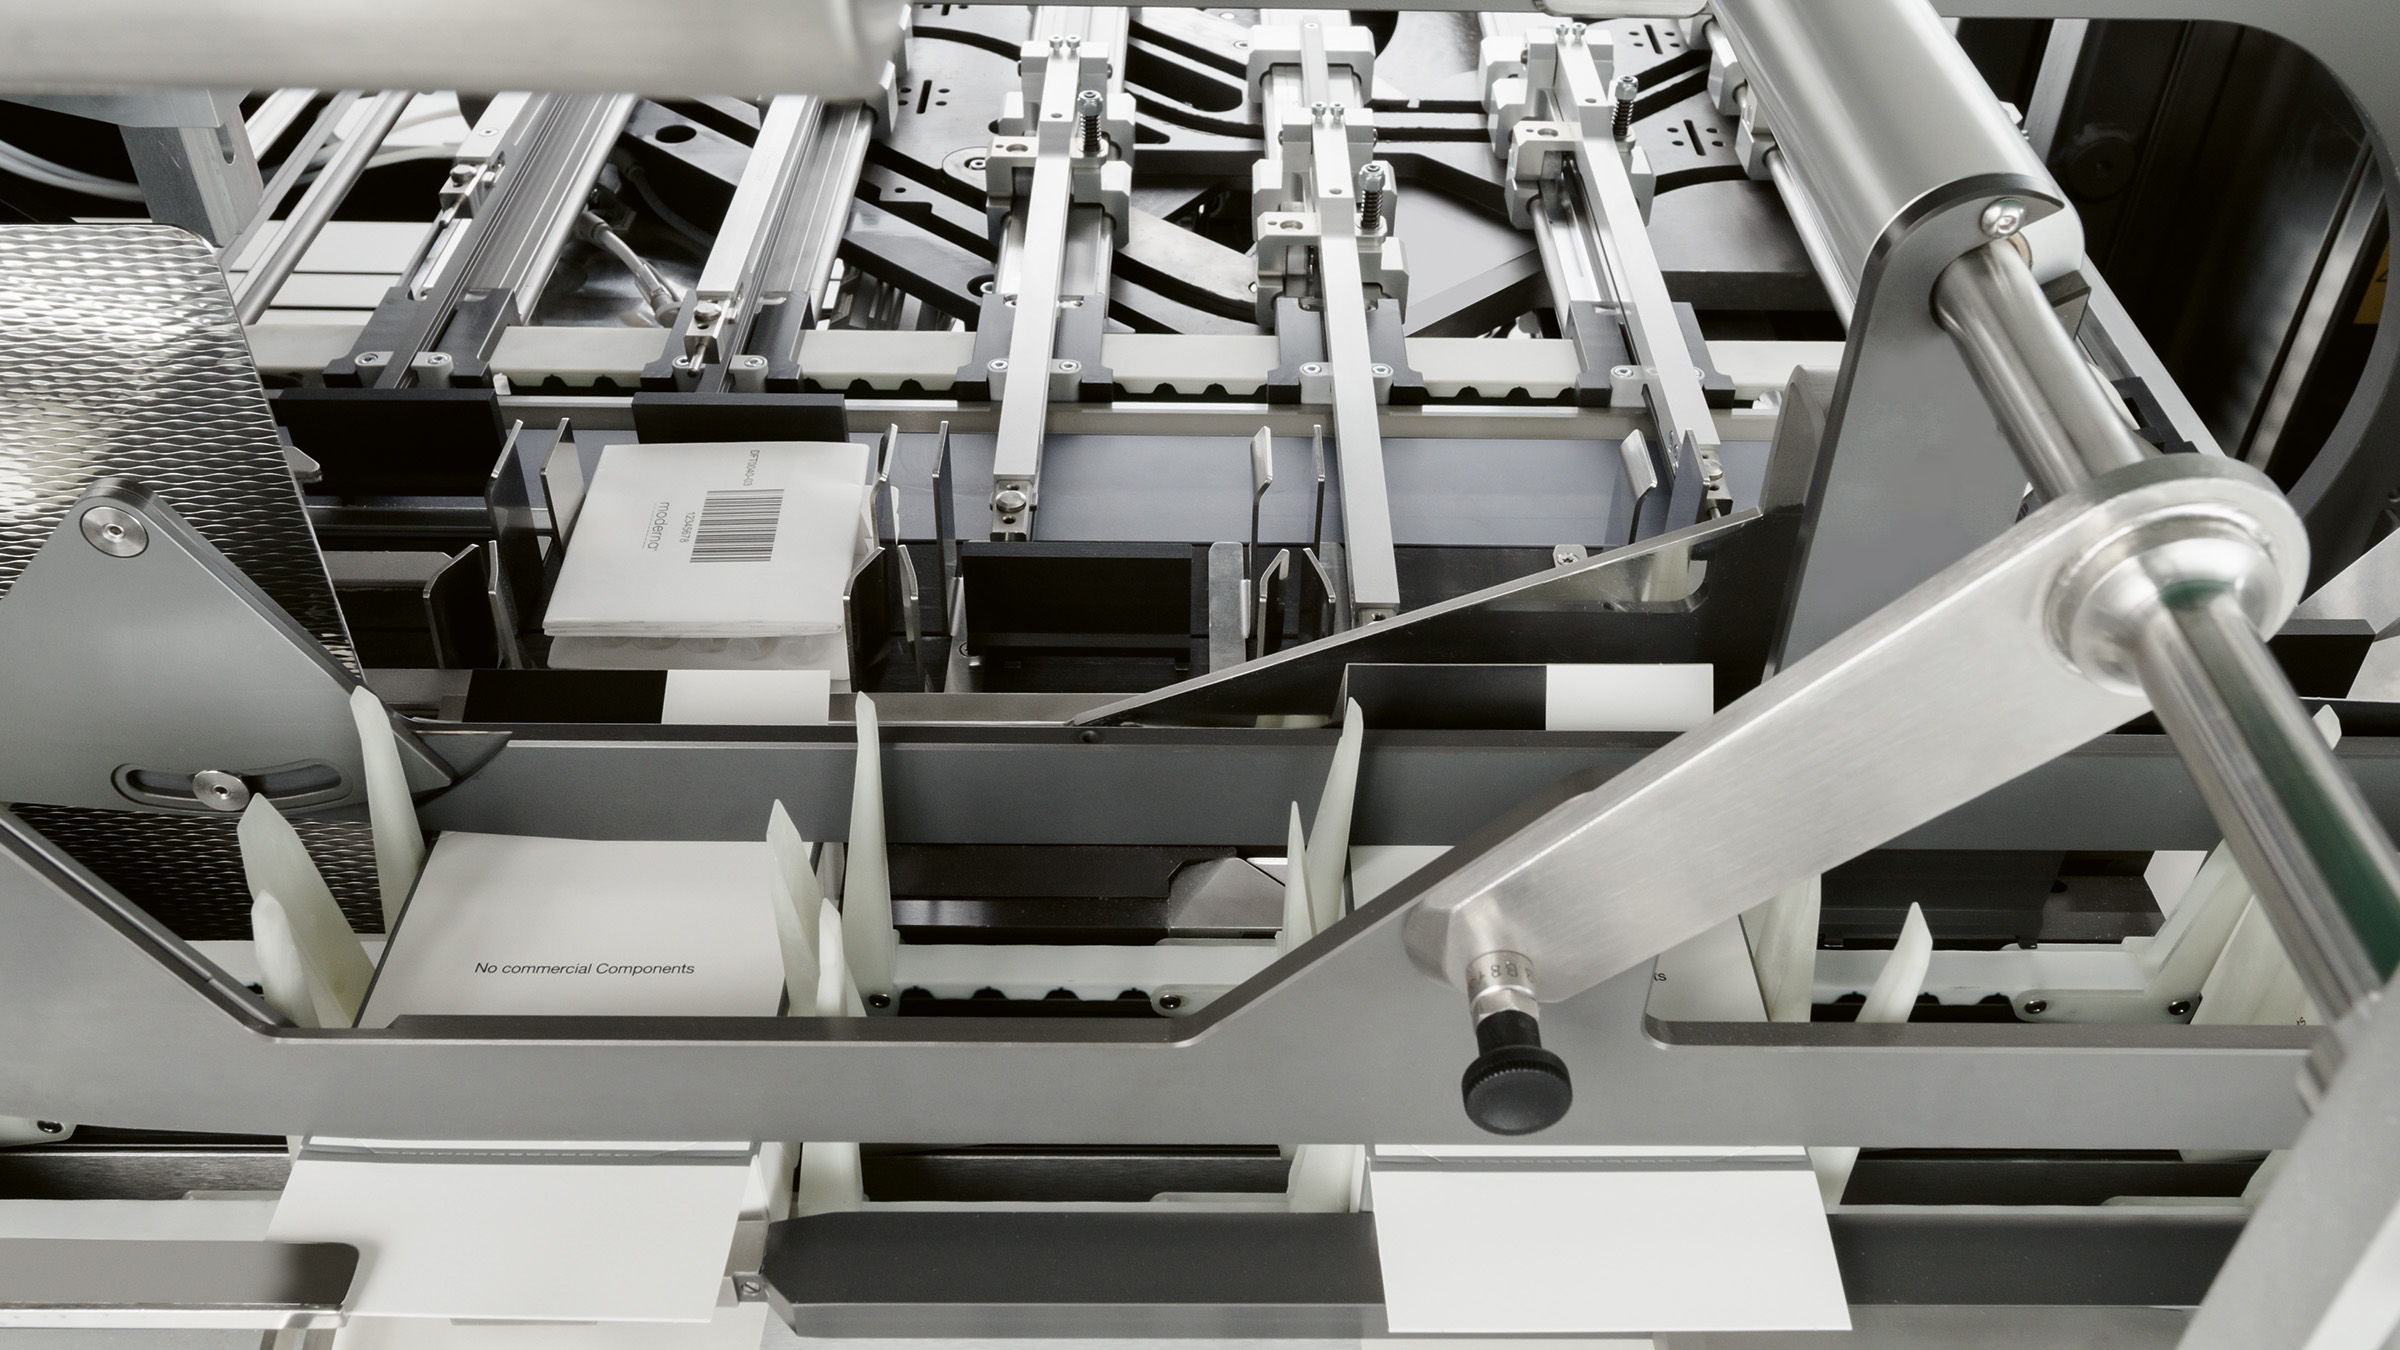
For effervescent tablet packaging lines, IMA Safe is able to provide complete cartoning solutions designed to flexibly support every customer requirement throughout the entire production process. The goal is to ensure maximum adaptability, operational continuity and seamless integration within different packaging line configurations.
In this context, IMA Safe offers a wide range of solutions covering different speed levels, in order to meet specific production requirements. The portfolio ranges from lower-speed solutions, such as the X Series, up to high-performance machines like the DYNAMICA Series, developed to guarantee maximum productivity.
Each solution is designed to ensure reliability, efficiency and ease of operation, while consistently maintaining high process quality according to the customer’s needs.
Labelling – IMA Life
Prioritising performance, precision and flexibility, HYPER stands out as one of the most advanced labelling solutions on today’s market, unbeatable in implementing brushless technologies, container positioning and label application. Moreover, HYPER handles almost any container type, material, shape and size, plus it applies plastic or paper labels and outserts. HYPER also features serialisation capabilities enabling Track & Trace for single containers, with the possibility of including overprinting devices and vision systems to read and check data.
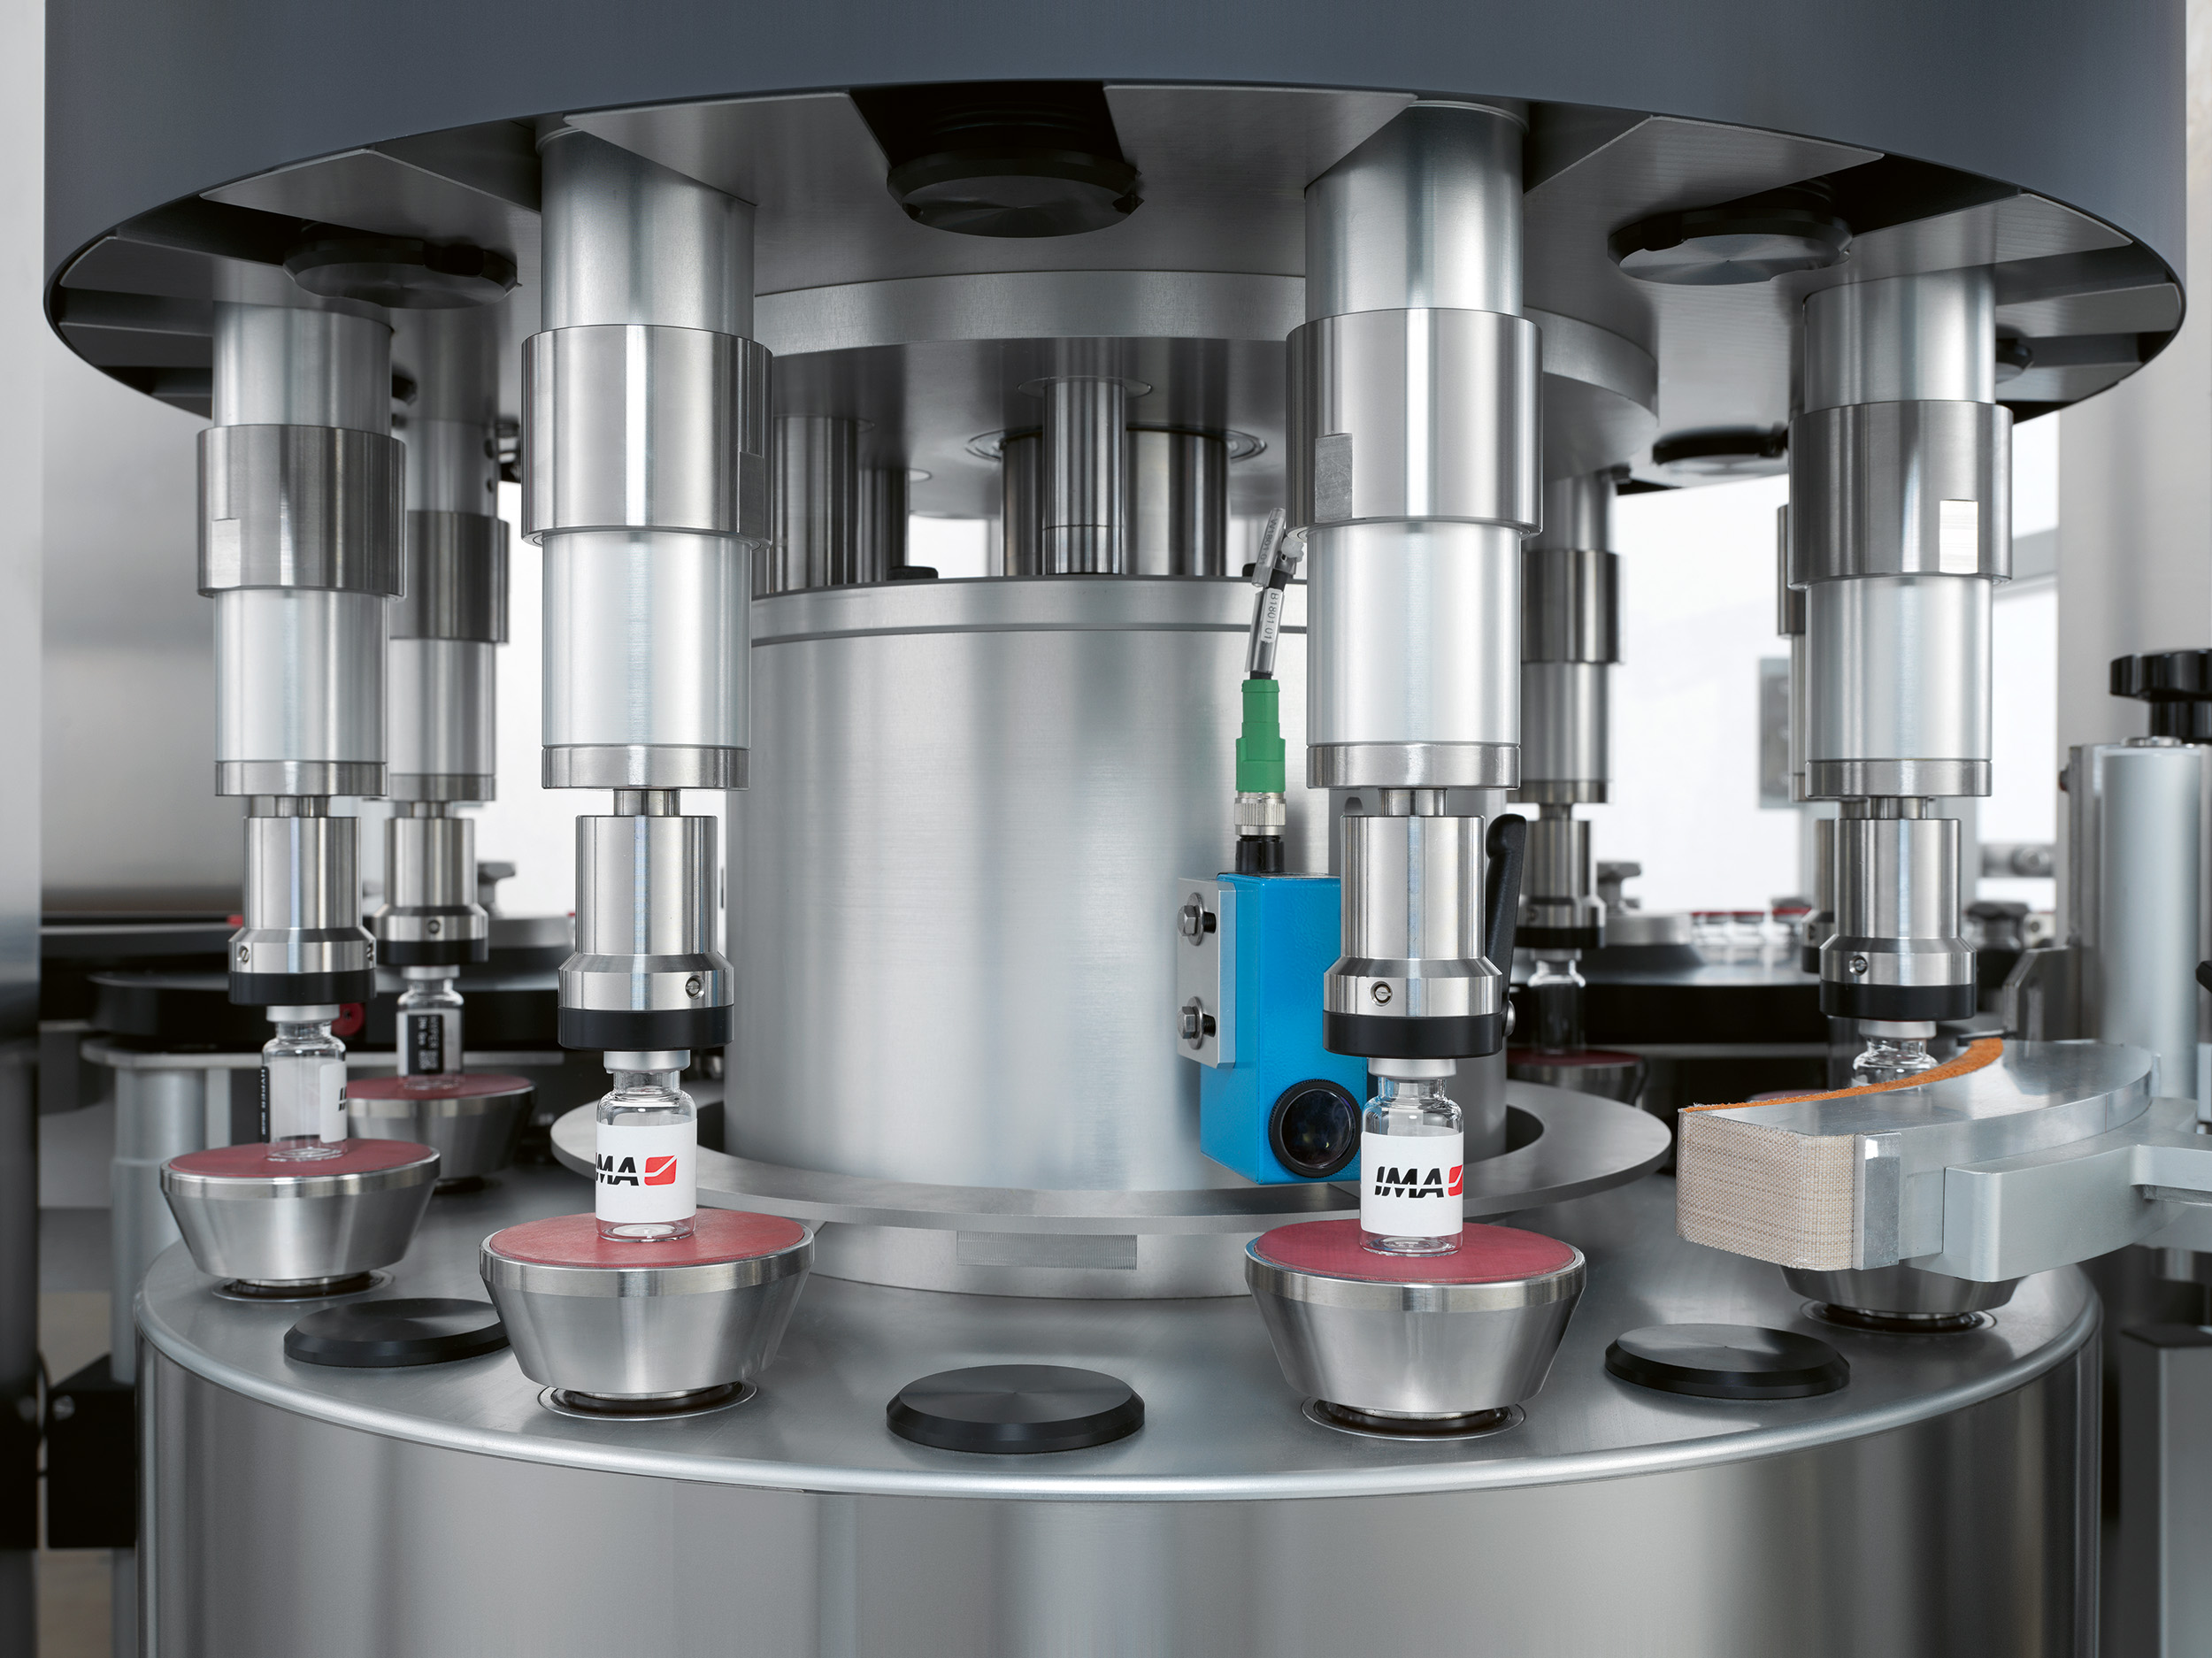
IMA Life’s SENSITIVE AP400 labelling solution is available with key features and design aspects that have been created to facilitate the operator’s tasks throughout the entire process, while ensuring the superior performance and versatility of a labeller that has already encountered widespread success in the pharmaceutical sector.
Transparent on three sides, operators are always able to closely monitor the labelling process, and the large front panels provide excellent access for cleaning and maintenance. The sliding reel holder, at a convenient height of 790 mm from ground level, makes changeover operations comfortable and swift, and the labelling process runs uninterrupted increasing productivity.
End of Line Operations – IMA BFB
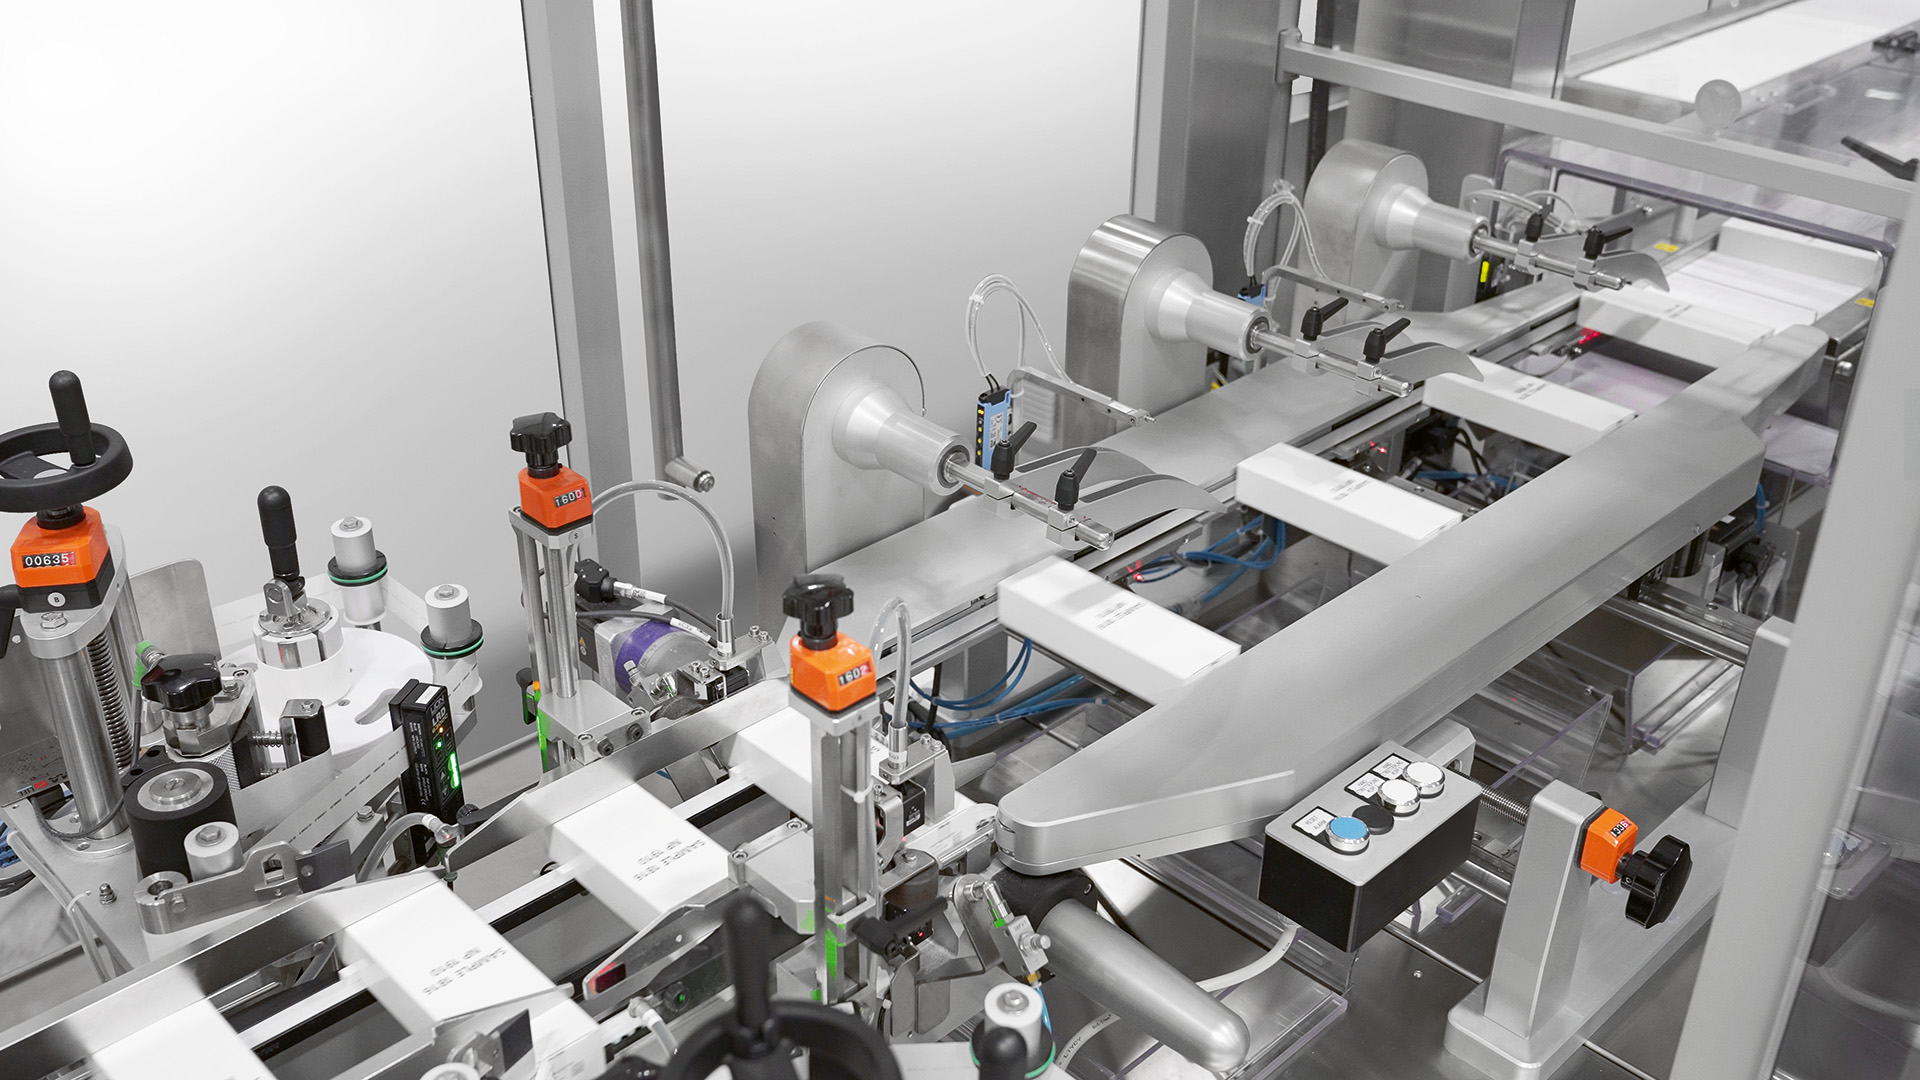
In the secondary packaging area, case packing solutions are available in multiple configurations, including side loading, top loading and wrap-around systems. These are supported by machines such as CPH2, CPV15/20, and MMP400, ensuring flexibility across different product types, formats and production speeds. These technologies make it possible to pack products into standard RSC cases for transport or into display-ready formats such as trays and wrap-around packs, supporting both logistics efficiency and shelf presentation.
At the end of the line, palletizing is managed through advanced automated systems such as RP2 and RP4. These solutions can be configured according to the required level of automation and may include features such as layer forming, pallet handling and storage, integration with AGVs, as well as labelling and weighing systems, ensuring a totally efficient and connected end-of-line process.
The power of cross-divisional synergy: IMA as an All-In-One Supplier
As the effervescent market continues to grow, manufacturers increasingly seek turnkey solutions that deliver speed, flexibility and product protection. IMA meets these expectations with integrated, customisable lines powered by the synergy of IMA Active, IMA Safe, IMA Life and IMA BFB. With this cross-divisional collaboration, customers can rely on a single partner capable of managing every stage of production – from powder processing and compression to packaging, labelling and end-of-line automation.
This All-In-One approach provides clear and measurable advantages: optimal machine compatibility, reduced engineering and project complexity, faster commissioning, and consistently higher efficiency and reliability across the entire line. Discover how IMA can support your next project: your future in effervescent starts here.

New
On show
Tableting
Up to 576,000 tabs/h
IMA S.p.A. – Active Division
Cartoning
Up to 400 cartons/min
Pack style: Carton

IMA S.p.A. – Safe Division
Labelling
Pack style: Bottle, Vial

IMA S.p.A. – LIFE Division Calenzano
New
Labelling
Pack style: Bottle, Vial

IMA S.p.A. – LIFE Division Calenzano
Case Packing
Pack style: Case/Shipper

IMA S.p.A. – BFB Division
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
11 min
White paper
ARCA: AI Root Cause Analysis.
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
13 min
Brands: IMA S.p.A. – Active Division, IMA Active
7 min
Brands: IMA S.p.A. – Active Division, IMA Active
12 min
Brands: IMA S.p.A. – Active Division
11 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Vitabalans Oy chooses PREXIMA.
4 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
The Energy Diary: powering sustainability.
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
10 min
Brands: IMA Active, IMA S.p.A. – Active Division
12 min
Brands: IMA Active, IMA S.p.A. – Active Division
8 min
Brands: IMA S.p.A. – Active Division, IMA Active
10 min
Brands: IMA S.p.A. – Active Division, IMA Active
10 min
Brands: IMA Active, IMA S.p.A. – Active Division
14 min
Brands: IMA Active, IMA S.p.A. – Active Division
15 min
Brands: IMA S.p.A. – Active Division, IMA Active
10 min
Brands: IMA S.p.A. – Active Division, IMA Active
12 min
Brands: IMA S.p.A. – Active Division, IMA Active
11 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Algorithm: «Why we choose IMA».
3 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Mastering tablet manufacturing: how segment tools improve productivity, efficiency and consistency.
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
34 min
Brands: IMA Active, IMA S.p.A. – Active Division
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
Comparison of minitablets and pellets as multiparticulate drug delivery systems for controlled drug release.
24 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Lubricant sensitivity of direct compression grades of lactose in continuous batch tableting process.
33 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
9 min
Brands: IMA Active, IMA S.p.A. – Active Division
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
14 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
11 min
Brands: IMA Active, IMA S.p.A. – Active Division
9 min
Brands: IMA Active, IMA S.p.A. – Active Division
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Formulation development of Vitamin C based effervescent blend suitable for direct compression.
9 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Capsule Orientation

3 min
Brands: IMA S.p.A. – Coffee Division
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
13 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
Autoregulation function on DOMINA tablet press.
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
10 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Power to the essential.
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
Preliminary results of predictive maintenance algorithms on a tablet press production machine.
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
The Prexima challenge. Comparison of rotary tablet presses seminar in Leverkusen (Germany).
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Directly compressed minitablets coated in a solid wall pan for the sustained release of drugs.
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
ARIA fluid bed granulator and MicroNIR
8 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
White paper
How to perform a good scale-up.
6 min
Brands: IMA S.p.A. – Active Division, IMA Active
White paper
Salty compression.
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
4 min
Brands: IMA Active, IMA S.p.A. – Active Division
6 min
Brands: IMA Active, IMA S.p.A. – Active Division
7 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Labelling & Serialization Integration

10 min
Brands: IMA Life
Case study
Tableting at its best.
5 min
Brands: IMA Active, IMA S.p.A. – Active Division
3 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
Together again: Chinoin chooses IMA.
4 min
Brands: IMA Active, IMA S.p.A. – Active Division
Case study
BMP: «PREXIMA fits all our needs».
4 min
Brands: IMA Active, IMA S.p.A. – Active Division
5 min
Brands: IMA Active, IMA S.p.A. – Active Division